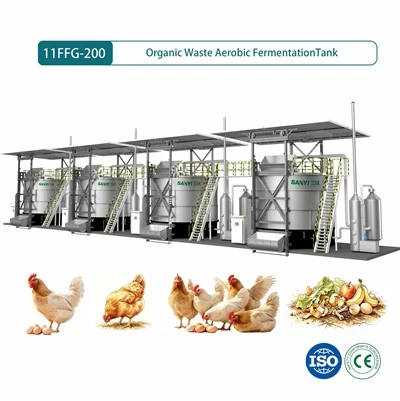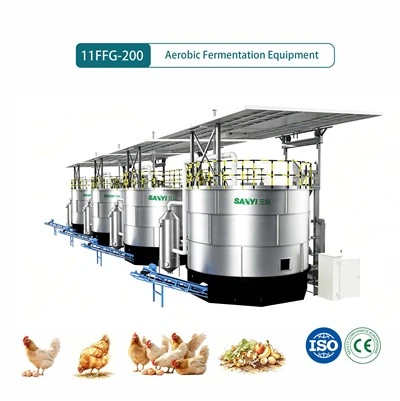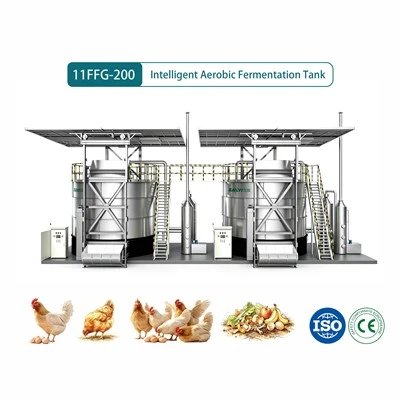

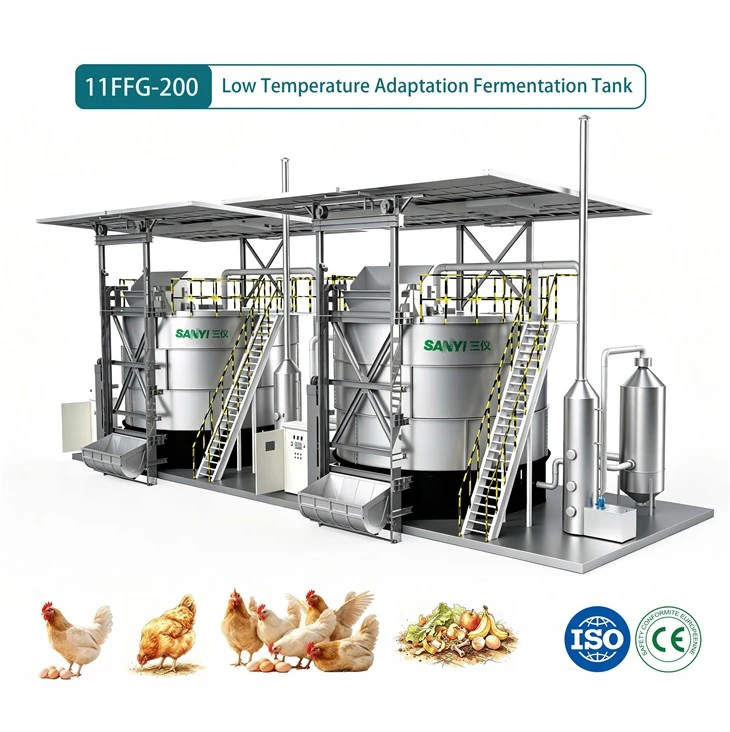


Shandong Heze Sanyi Biological Engineering Co., Ltd. is one of the leading manufacturers and suppliers of low temperature adaptation fermentation tank in China. With abundant experience, we are committed to providing high quality equipment made in China with competitive price. Welcome to buy durable low temperature adaptation fermentation tank from our factory. Customized orders are welcome.
Product Overview
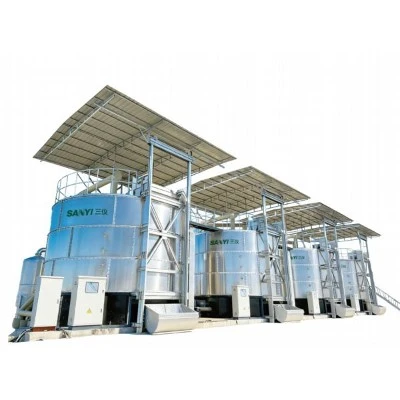
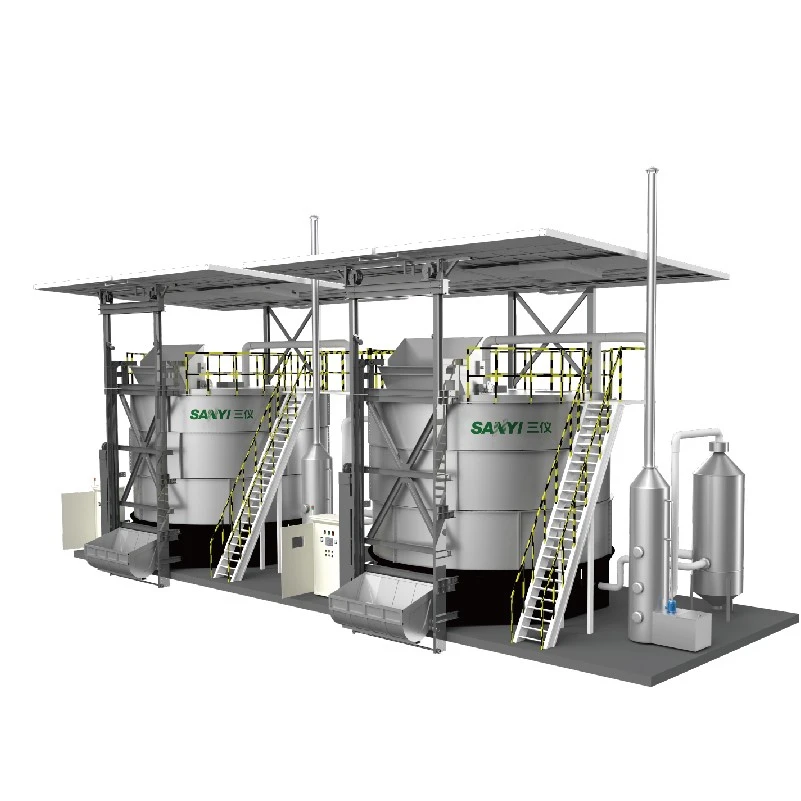
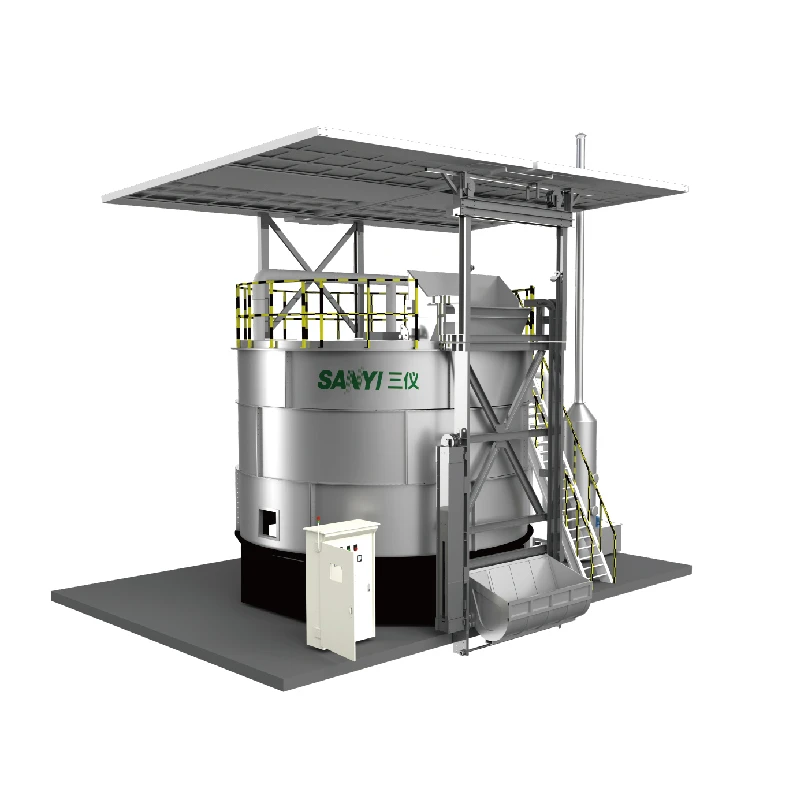
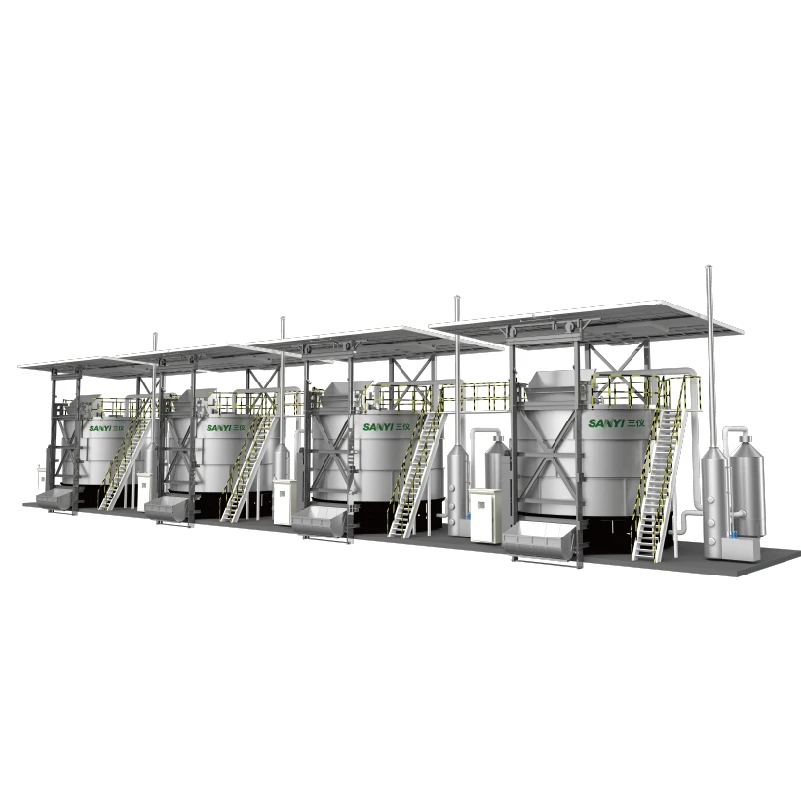
The low-temperature adaptable fermentation tank is an intelligent aerobic fermentation equipment specially developed by Sanyi for organic waste treatment under extreme low temperatures, which fundamentally solves the problem of fermentation stagnation caused by temperature drop in winter in high-latitude and northern frigid regions. The equipment adapts to ambient temperature ranging from -30℃ to 40℃, serving as a special model for alpine pastures, northern livestock breeding bases, northern sludge and kitchen waste treatment projects. It inherits the basic vertical sealed structure supporting direct fermentation without auxiliary materials, capable of treating chicken manure, pig manure, sludge, dead livestock and kitchen waste. Raw materials with moisture content ≤75% can be directly fed without conditioning materials. Equipped with four core energy-saving and heat preservation technologies for low temperature adaptation and a full set of PLC intelligent control system, the tank can stably maintain high fermentation temperature above 65℃ even under -30℃ extreme cold environment, completing sterilization and decomposition within 7–10 days, and the produced organic fertilizer complies with NY525-2021 standard. All heat preservation, heat exchange, heating and stirring components of the whole machine are upgraded for low temperature resistance. Low-temperature resistant steel, thickened high-density insulation layer and high-efficiency countercurrent heat exchange modules work together to significantly reduce energy consumption in winter, realizing uninterrupted continuous fermentation production all year round and solving the pain points of traditional fermentation equipment such as winter shutdown, incomplete fermentation and sharp capacity decline.
Core Components & Accessories (Special Upgraded Version for Low Temperature)
Ultra-thick Multi-layer Insulated Fermentation Tank (Customized for Low Temperature)
The inner wall uses 3mm national standard 304 stainless steel plate, and the outer wall adopts thickened 201 stainless steel load-bearing steel plate. The interlayer is filled with ≥50mm high-density polyurethane insulation layer (density ≥40kg/m³), equipped with multi-layer load-bearing frames and full laser welding sealing, greatly improving temperature locking capacity to isolate internal high temperature loss and resist external sub-zero cold invasion.
Low-temperature Special High-strength Stirring Assembly
Stirring blades are bent and fully welded with Q355E low-temperature high-strength structural steel, fully covered with 2–3mm 304 stainless steel anti-corrosion layer externally, with lengthened and thickened reinforcing base plates at the bottom. The steel will not brittle crack and load capacity will not decline under low temperature. The 42CrMo tempered ratchet and Q355 seamless main shaft adopt low-temperature tempering process to adapt to extreme sub-zero working conditions.
Four-fold Energy-saving Waste Heat Recovery Heat Exchange System (Core Low-temperature Accessory)
Adopts honeycomb fin tube countercurrent U-shaped heat exchange structure with ultra-high thermal conductivity stainless steel heat exchange components, boosting heat exchange efficiency by 300% compared with traditional equipment. It can preheat outdoor fresh air at -30℃ to 5℃ before feeding into the tank for oxygen supply, greatly cutting auxiliary heating energy consumption. Matched with high-power dual-mode electric/steam auxiliary heating module to rapidly raise temperature at low-temperature startup stage and avoid fermentation stagnation.
Low-temperature Adaptable PLC Intelligent Temperature Control System
Siemens PLC intelligent control cabinet is equipped with low-temperature special temperature sensing probes to accurately identify temperature difference under sub-zero environment. The system adds exclusive low-temperature temperature control programs, which automatically increase waste heat recovery power, activate auxiliary heating in advance and extend aeration & stirring duration to intelligently match fermentation technology for alpine regions. It supports remote monitoring, low-temperature fault early warning and one-key anti-freezing protection.
Anti-freezing Multi-stage Deodorization System
Pipeline tracing and heat preservation devices are installed for spray, pickling and ozone oxidation towers to prevent pipeline icing and blockage in winter, ensuring continuous and stable odor purification under frigid weather and all-day standard exhaust discharge.
Anti-freezing Hydraulic Feeding & Discharging Mechanism
The hydraulic station is filled with low-temperature special hydraulic oil and equipped with pipeline heat tracing. The hydraulic lifting and discharging transmission operate smoothly without jamming at -30℃ to guarantee continuous daily feeding and discharging.
Process & Core Advantages
- Extreme Cold Waste Heat Recovery & Heat Exchange Process (Core Patented Technology) High-temperature fermentation tail gas conducts countercurrent heat exchange with outdoor cold air to recover waste heat for air preheating. Fresh air at -30℃ can be preheated to 5℃, directly reducing auxiliary heating energy consumption by 50%, and the overall energy-saving rate of the whole machine reaches 40%, ranking at the leading level among similar products.
- Multi-layer High-density Tank Temperature Locking & Insulation Process ≥50mm high-density polyurethane insulation interlayer matched with multi-layer load-bearing sealing frames, full internal and external welding isolates heat and cold conduction, cutting internal high temperature loss by 70%, eliminating the need for full-time high-power heating to maintain fermentation temperature.
- Low-temperature Resistant Steel Forging Process Stirring parts, main shaft and transmission ratchets are all made of low-temperature impact-resistant steel with low-temperature tempering quenching & tempering process, free from cold brittleness, deformation and fracture at -30℃ for stable heavy-load operation all year round.
- Alpine Exclusive Intelligent Anti-freezing Temperature Control Process The PLC is embedded with exclusive low-temperature fermentation programs, which monitor ambient temperature and internal tank temperature difference in real time and automatically link heat exchange, auxiliary heating, aeration and stirring for coordinated regulation. An anti-freezing protection program will be automatically triggered during low-temperature shutdown to prevent tank and pipeline freeze damage.
- Comprehensive Product Advantages Suitable for frigid regions down to -30℃ with uninterrupted production all year round, completely solving the problem of fermentation paralysis in northern winter. Four overlapping energy-saving technologies sharply reduce winter operation cost. All spare parts are specially reinforced for low temperature, extending service life and lowering failure rate. It retains all advantages of vertical sealed structure, fermentation without auxiliary materials, automatic remote control and multi-stage environmental deodorization. Each unit covers 70–105 ㎡ with a 15-day fermentation cycle to realize daily feeding and discharging, being the preferred equipment for resource utilization of organic waste in alpine cold regions.
Hot Tags: low temperature adaptation fermentation tank, China low temperature adaptation fermentation tank manufacturers, factory