


Shandong Heze Sanyi Biological Engineering Co., Ltd. is one of the leading manufacturers and suppliers of intelligent aerobic fermentation tank in China. With abundant experience, we are committed to providing high quality equipment made in China with competitive price. Welcome to buy durable intelligent aerobic fermentation tank from our factory. Customized orders are welcome.
Product Overview
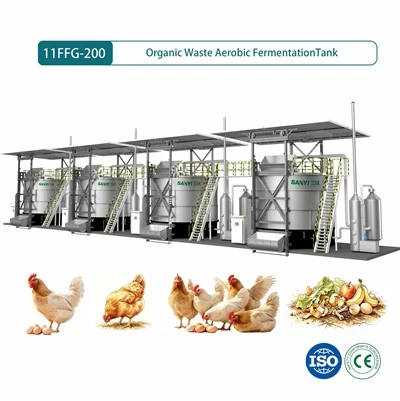
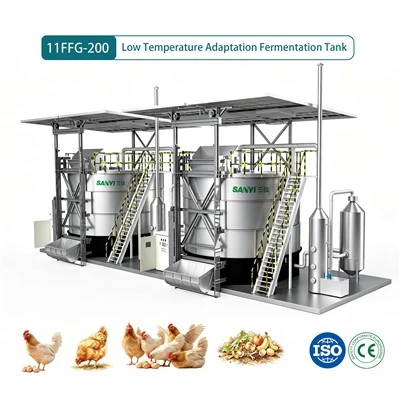
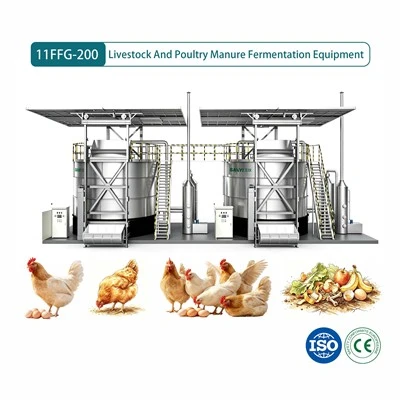
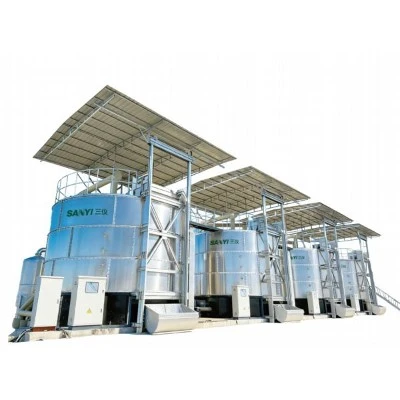
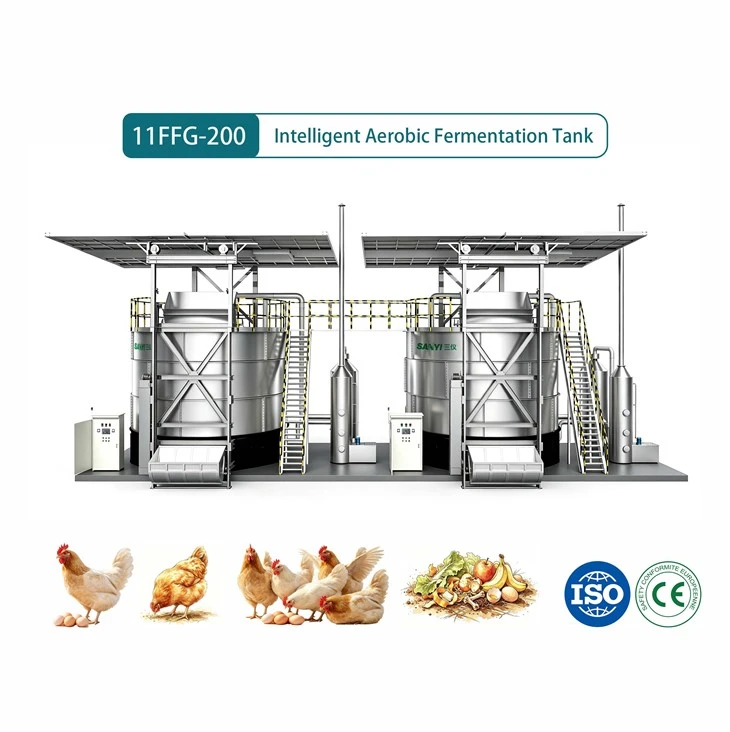
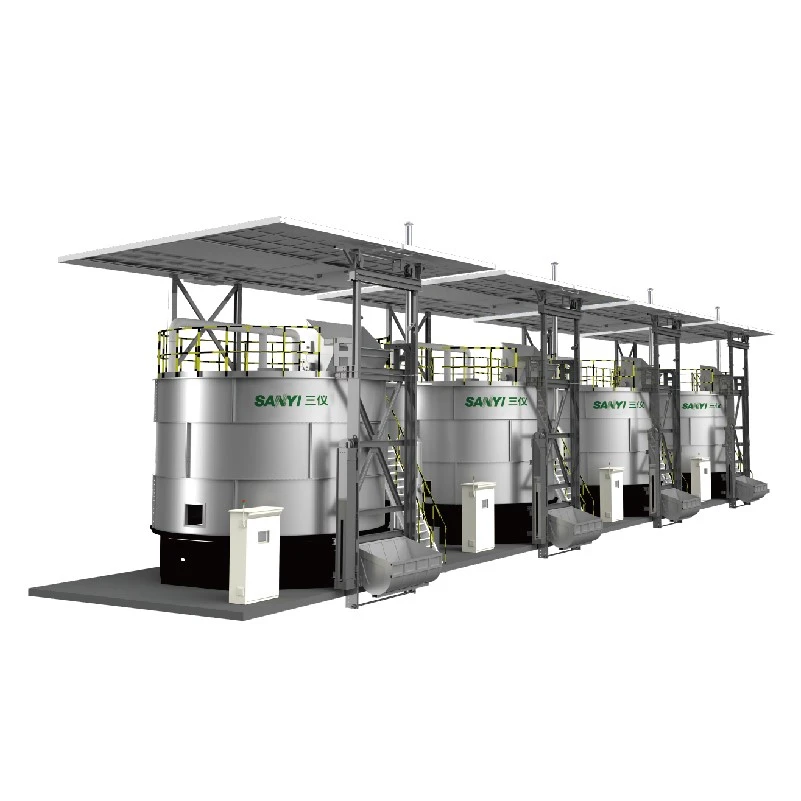
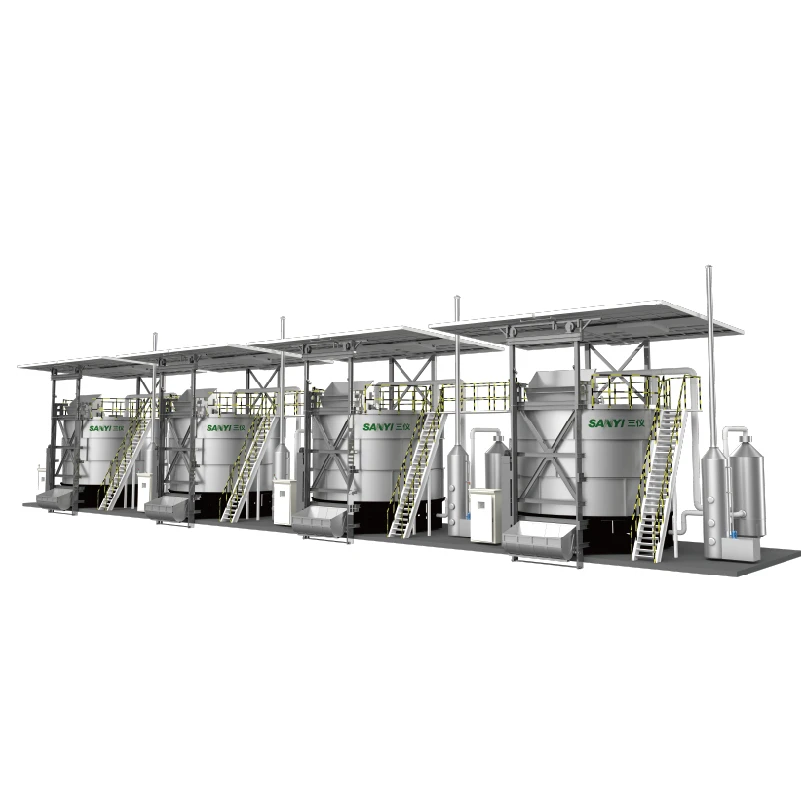
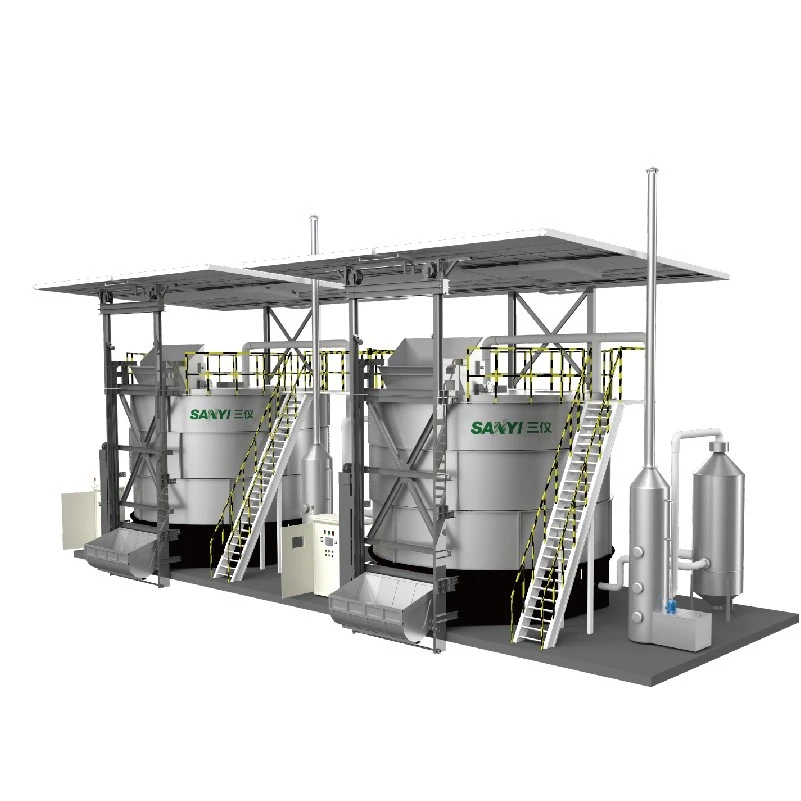
The intelligent aerobic fermentation tank is an integrated intelligent control model of complete organic waste treatment equipment, focusing on full-process automatic management. Equipped with a full set of PLC programmable intelligent control system based on standard fermentation tank structure, it provides unattended manure fermentation solutions for large-scale farms, kitchen waste disposal centers and sludge treatment stations. The equipment can treat multiple types of organic waste including livestock manure, dead animals, municipal sludge and kitchen waste. Raw materials with moisture content below 75% can be fermented directly without auxiliary materials. Supported by intelligent sensors and remote control technology, it automatically regulates the whole processes of aeration, stirring, heating, discharging and deodorization without real-time manual attendance, and one operator can remotely manage multiple tanks. The fermentation temperature is stably maintained at 65–75℃, and the finished organic fertilizer meets NY525-2021 standard. It integrates multiple advantages including small sealed floor space, high automation, stable operation, convenient maintenance and environmental compliance, suitable for four-season conventional climate scenarios, serving as core intelligent equipment for modern circular agriculture and environmental solid waste treatment projects.
Core Accessories
Vertical Double-layer Insulated Fermentation Tank Body
304 stainless steel inner lining + 201 stainless steel outer wall + polyurethane insulation interlayer, sealed by full laser welding with excellent anti-corrosion and heat preservation performance for long-term continuous fermentation.
High-strength Stirring Transmission Assembly
Q355 seamless steel pipe main shaft, thickened stirring blades fully covered with 304 stainless steel, integrally forged 42CrMo alloy steel ratchet, featuring heavy load resistance, fatigue resistance, corrosion resistance, deformation and fracture prevention.
PLC Intelligent Central Control System (Core Accessory)
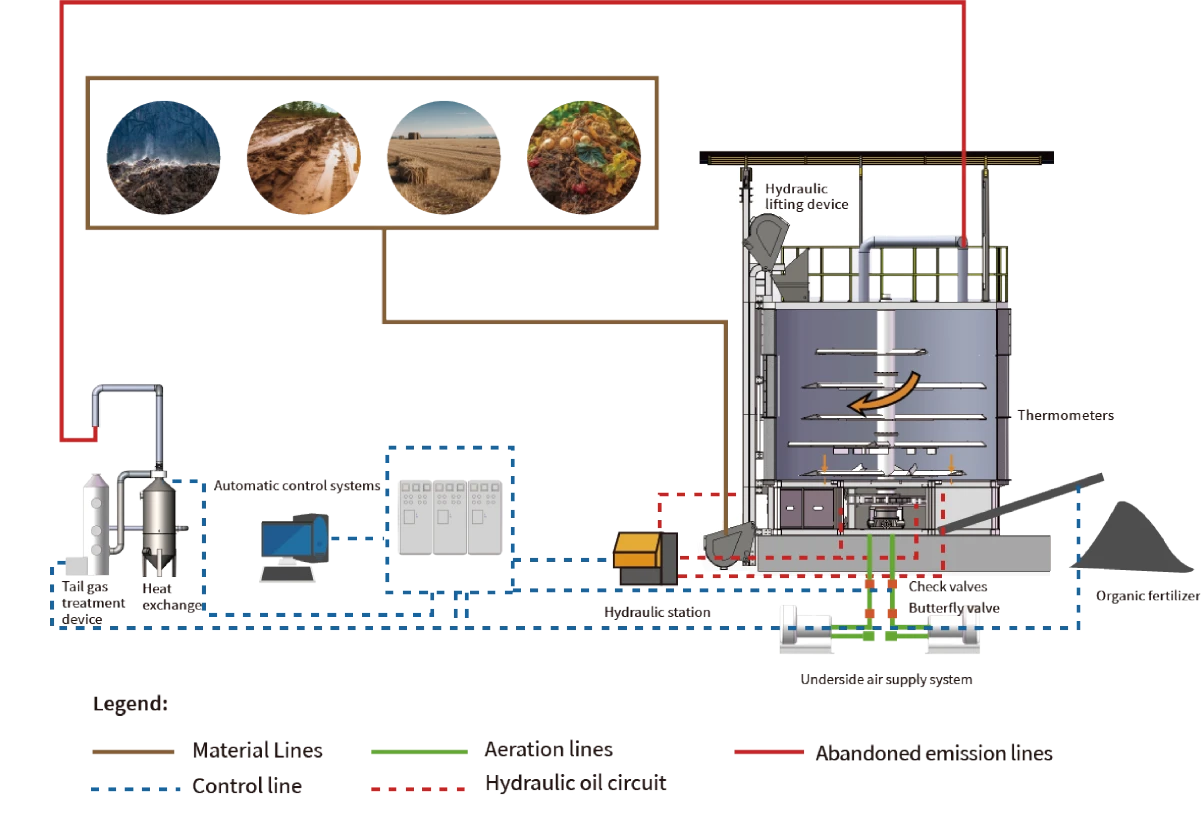
Adopts Siemens programmable logic controller with large touch screen, integrated high-precision sensors for temperature, humidity, oxygen concentration and pH value to collect real-time operation data inside the tank. Five core intelligent functions: one-key start-stop, automatic sound-light fault alarm, automatic whole-process data recording and storage, self-defined parameter adjustment, remote online control via mobile phones and computers.
Intelligent Constant Temperature Heat Exchange & Auxiliary Heating System
Equipped with automatic waste heat recovery heat exchange module. The system automatically adjusts fresh air flow and auxiliary heating power according to material temperature inside the tank. Fermentation waste heat recycling achieves over 30% energy saving, and electric/steam heating will be automatically activated when temperature is insufficient to maintain suitable metabolic environment for microorganisms.
Fully Automatic Multi-stage Deodorization Unit
Matched with automatic dosing spray tower, pickling tower and saturated ozone oxidation treatment tower. The system automatically adjusts spray dosage and ozone generation power based on odor concentration to complete exhaust purification without manual intervention, ensuring stable standard discharge of tail gas.
Automatic Hydraulic Feeding & Discharging Assembly
The intelligent hydraulic station links lifting feeder and discharging conveyor, automatically triggering feeding and discharging procedures according to fermentation cycle. The centralized lubrication system regularly injects oil automatically to maintain transmission parts.
Process & Core Advantages
- Full-process Intelligent Automatic Regulation Process Driven by PLC intelligent core to link all equipment units, eliminating manual adjustment of aeration duration, stirring frequency and heating power. Sensors feed back material status in real time, and the system independently matches optimal fermentation process parameters to greatly improve fermentation stability.
- Remote Online Monitoring & Maintenance Process Support remote login via mobile terminals and computers to view real-time operation data, historical fermentation records and fault codes. Remote start-stop and parameter modification can be realized off-site, eliminating the need for permanent operators in remote factories and greatly cutting labor costs.
- Intelligent Constant Temperature Energy-saving Fermentation Process Combined waste heat recovery and intelligent variable frequency auxiliary heating enable precise temperature control to avoid invalid heating energy consumption, saving 30%–40% energy under normal working conditions. Fermentation will not be affected by small day-night temperature fluctuations.
- Automatic Multi-stage Deodorization Purification Process The dosage of chemicals and ozone is automatically adjusted linked with odor concentration to avoid chemical waste, stabilize purification efficiency and eliminate the risk of excessive tail gas caused by manual operation errors.
- Comprehensive Product Advantages Leading intelligent level in the industry, one-key operation lowers operation threshold, new operators can get started after simple training. Strong anti-interference ability ensures stable operation and low failure rate. Compact vertical sealed structure occupies small space with 15-day fermentation cycle for continuous production. Complete intelligent data recording facilitates standardized production management and environmental account retention. Full set of automatic mechanisms reduce manual contact with manure and improve workshop working environment.
Hot Tags: intelligent aerobic fermentation tank, China intelligent aerobic fermentation tank manufacturers, factory