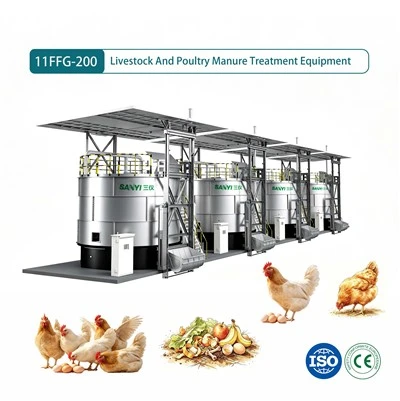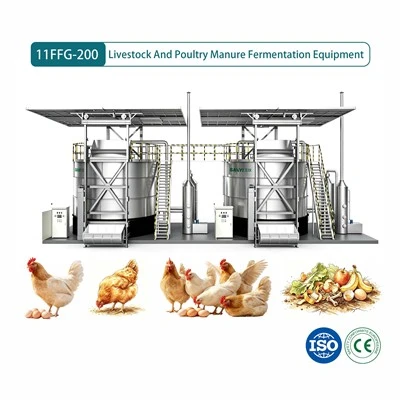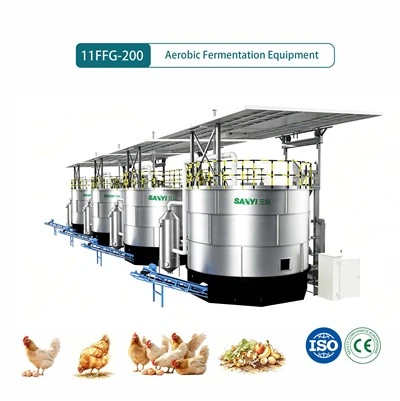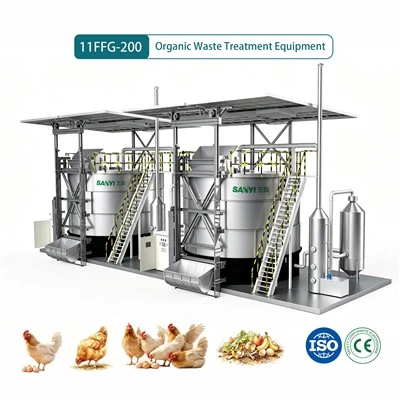


Shandong Heze Sanyi Biological Engineering Co., Ltd. is one of the leading manufacturers and suppliers of energy-saving fermentation tank in China. With abundant experience, we are committed to providing high quality equipment made in China with competitive price. Welcome to buy durable energy-saving fermentation tank from our factory. Customized orders are welcome.
Product Overview
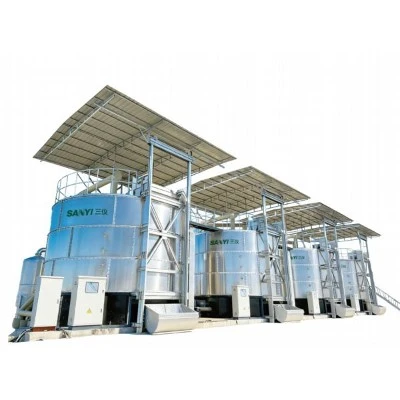
Energy-saving & Carbon-reduction Vertical Intelligent Aerobic Fermentation Tank (Version 2.0) is a new-generation low-consumption organic waste composting equipment independently developed by Shandong Heze Sanyi Biological Engineering Co., Ltd. It targets large-scale livestock farms, sludge disposal stations and kitchen waste treatment centers. Equipped with four original energy-saving technology systems, it cuts annual power consumption significantly compared with traditional V1.0 tanks and achieves a 40% carbon emission reduction per unit annually, solving high fan power loss, transmission energy waste, waste heat loss and idle power consumption of conventional fermenters. Adopting vertical fully sealed double-layer insulated tank structure, it directly accepts raw materials with moisture content ≤75% without auxiliary materials. Continuous thermophilic fermentation at 65–75 ℃ lasts 5–7 days to thoroughly eliminate parasite eggs and pathogenic bacteria. The finished organic fertilizer complies with NY525-2021 national standard. It adapts to cold and humid regions and minimizes floor space via vertical layout.


Core Accessories
Zero-friction Aeration Blower System
Contactless bearing design with transmission efficiency ≥98%, cutting power consumption by 50% under identical oxygen supply conditions, wear-free and low-noise for stable long-term oxygen supply;
Direct-drive & Direct-coupled Transmission Assembly
Eliminates redundant reducers and couplings to shorten power transmission chain, reducing inherent energy loss by 15%;
Counter-flow Bidirectional U-type Waste Heat Exchanger
Total heat exchange area of 210 ㎡, waste heat recovery efficiency 300% higher than traditional structures; recovered heat circulates to heat the tank and cuts heating power consumption sharply;
Intelligent PLC Energy-saving Control Cabinet
Collects real-time data of oxygen, temperature, humidity and stirring speed; algorithms dynamically adjust operation conditions to avoid idle power waste;
Anti-corrosion Tank Assembly
Inner wall with 3mm national standard 304 stainless steel, outer wall with thickened 201 stainless steel, double-layer polyurethane insulation locks fermentation heat and reduces heating startup frequency;
High-strength Mixing Shaft & Blades
Main frame of Q355 structural steel with 304 anti-corrosion contact surface; 42CrMo alloy forged ratchet wheel resists deformation under heavy continuous load and ensures uniform mixing for microbial fermentation.
Process & Energy-saving Advantages
- Ultra-low Energy Consumption & Carbon Reduction: Four energy-saving technologies work together to reach a comprehensive energy-saving rate of 40%. Traditional tanks consume 419,000 kWh per year while this model only uses 241,000 kWh, cutting carbon emission by 101 tons per unit yearly, ideal for carbon-neutral livestock projects;
- Recyclable Waste Heat: Full recovery of exhaust waste heat for self-heating, eliminating extra high-power heating devices in cold winter;
- Ultra-low Operation Loss: Zero-friction blower and streamlined transmission double the service cycle of vulnerable parts and lower maintenance cost;
- Odor-free Fully Sealed Design: Vertical closed tank collects all waste gas for centralized treatment with no odor leakage and secondary pollution;
- Fully Automatic Labor-saving Operation: One-key start-stop, automatic fault alarm and data recording, no 24-hour on-site operator required;
- Wide Raw Material Adaptability: Directly processes chicken manure, pig manure, livestock carcasses, municipal sludge and kitchen waste without straw, sawdust or other moisture-conditioning additives.

Hot Tags: energy-saving fermentation tank, China energy-saving fermentation tank manufacturers, factory